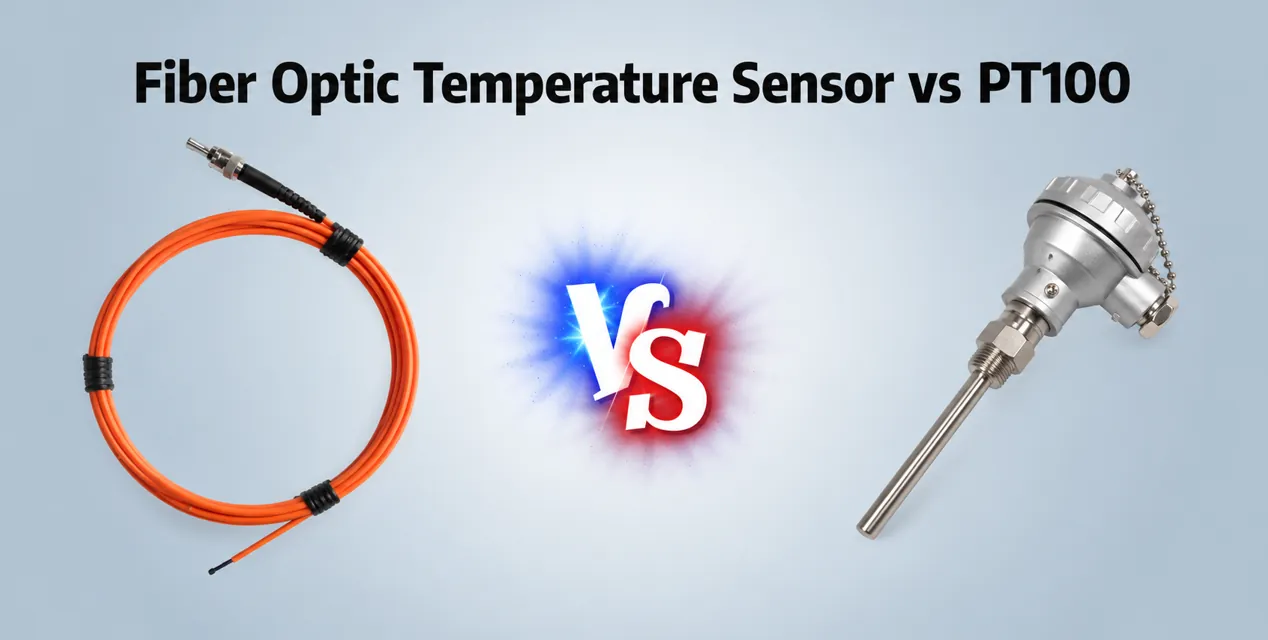
This comparison focuses on fluorescence-based point fiber optic temperature sensors and conventional PT100 resistance temperature detectors.
Fiber optic temperature sensors and PT100 sensors can both provide point temperature measurement, but they use very different sensing and signal-transmission methods. PT100 uses the predictable resistance change of a platinum element and requires electrical conductors between the sensing element and measurement electronics. A fiber optic temperature probe uses an optical sensing path and carries the measurement signal through optical fiber, making it useful where electrical isolation or immunity to electromagnetic interference is important.
PT100 is often a practical choice for conventional industrial temperature measurement. Fiber optic sensing becomes more attractive when the measurement point is inside or close to high-voltage equipment, strong electromagnetic fields, RF or microwave environments, strong magnetic fields, or electrically isolated structures.
Key Takeaways
PT100 is a mature and widely used resistance-based temperature sensor for conventional industrial measurement. Fiber optic probes provide an electrically isolated optical sensing path without conductive signal wiring at the measurement point. Strong EMI, high voltage, RF or magnetic fields can strongly influence which technology is more suitable. PT100 systems are usually straightforward for conventional process equipment and control panels. Fiber optic temperature sensing is particularly useful for transformer windings, energized equipment and other electrically sensitive locations. The final choice should consider not only temperature range and accuracy, but also installation location, wiring environment, number of sensing points and monitoring interface.
Fiber Optic Temperature Sensor vs PT100 at a Glance
| Comparison | Fiber Optic Temperature Sensor | PT100 |
|---|---|---|
| Measurement Principle | Optical point-temperature measurement | Platinum resistance temperature measurement |
| Signal Path | Optical fiber | Electrical lead wires |
| Electrical Conductivity | Non-conductive sensing path | Conductive sensing path |
| EMI / RFI Immunity | Optical signal path is inherently immune to EMI at the sensing link | Electrical wiring and measurement circuits may require suitable shielding and installation practices |
| High-Voltage Measurement | Suitable for direct measurement near energized structures | Suitable when insulation and wiring are properly designed |
| Strong Magnetic Fields | Not affected by magnetic field coupling along the fiber | May require additional shielding or routing consideration |
| Probe Size | Compact sensing tip, varies by configuration | Wide range of constructions, from compact elements to sheathed probes |
| Lead / Fiber Routing | Optical fiber routed from probe to instrument | Copper lead wires routed to transmitter or controller |
| Multi-Point Monitoring | Multiple probes connect to a multi-channel instrument | Multiple RTDs connect to multi-channel acquisition or control systems |
| Signal Conditioning | Requires a fiber optic temperature transmitter or monitoring instrument | Requires an RTD input module or temperature transmitter |
| PLC / SCADA Integration | Via RS485, Modbus, analog output or relay from the monitoring instrument | Via RTD input module or transmitter output |
| Typical Applications | Transformer windings, high-voltage equipment, RF/EMI-sensitive locations | Conventional industrial and process equipment |
How the Two Temperature Sensors Measure Temperature
Fiber Optic Temperature Sensor
Light is transmitted through an optical fiber to a defined probe tip, where the sensing takes place. The optical return signal travels back through the same fiber and is processed by a monitoring instrument, which converts it into a temperature reading. No electrical sensing signal is required at the measurement point itself.
PT100 Temperature Sensor
A PT100 element is made of platinum, whose electrical resistance changes in a predictable way with temperature. Measurement electronics apply a small current and calculate temperature from the resulting resistance value. Electrical lead wires connect the RTD element to the measuring instrument, forming a conductive circuit from the sensing point to the control room or panel.
Electrical Isolation and High-Voltage Environments
This is one of the most important distinctions between the two technologies. PT100 uses conductive wiring between the sensing element and the instrument. A fiber optic probe uses an optical path instead, so no electrical signal travels along the sensing link.
This distinction matters in locations such as transformer windings, high-voltage test equipment, energized electrical components, electrical insulation structures, and selected measurement points inside switchgear. PT100 can be used in many electrical applications when the installation, insulation and measurement circuit are properly designed. However, direct temperature measurement at locations requiring a non-conductive signal path may favor fiber optic sensing.
EMI, RFI and Strong Electromagnetic Fields
Fiber optic sensing does not use electrical signal transmission along the sensing fiber, so the optical path itself is not affected by electromagnetic coupling. PT100 relies on resistance measurement through conductive leads, so wiring method, shielding, grounding and instrumentation design can become more important in electrically noisy environments.
Typical environments where optical sensing may be preferred include transformer windings, generators, high-current bus systems, RF equipment, microwave heating installations, MRI systems, and high-voltage laboratories.
Temperature Range, Accuracy and Response Time
Both technologies can provide useful industrial temperature measurements, but actual performance depends on the sensor construction, the instrument and the application.
For a typical fiber optic point temperature probe, the usable range is commonly around -40 to 260 °C, with accuracy in the region of ±0.5 to ±1 °C and response times under 1 second, depending on probe configuration. PT100 sensors are available in many industrial constructions and temperature ranges, so the usable specification depends strongly on the RTD element, sheath, wiring and transmitter.
| Parameter | Fiber Optic | PT100 |
|---|---|---|
| Temperature Range | Depends on optical probe configuration | Depends on RTD construction |
| Accuracy | Depends on probe and instrument | Depends on RTD class, wiring and transmitter |
| Response Time | Small probes can respond quickly | Depends strongly on element and protective sheath |
| Signal Path | Optical | Electrical resistance |
Probe Size and Installation Space
Fiber optic temperature probes can use compact sensing tips, with typical probe diameters around 2–3 mm depending on configuration, which can be an advantage in restricted winding spaces. PT100 sensors are available in many physical constructions, from compact elements to metal-sheathed industrial probes, and can also fit a wide range of installation spaces.
The determining factor is not that one technology is always smaller — probe geometry must match the specific measurement point, its access, and its mechanical protection requirements.
Fiber Routing vs Electrical Wiring
Fiber Optic Probe
Optical fiber routing runs from the sensing point to the monitoring instrument. Lengths of around 3–5 m are commonly practical for many equipment installations, with longer fiber runs available where needed. Because the fiber carries an optical signal, it provides electrical isolation along the route and typically requires attention to bend radius and mechanical protection during installation.
PT100
PT100 sensors are wired using 2-wire, 3-wire or 4-wire measurement arrangements, with conductive cable routed from the sensing element to the instrument. Lead resistance can influence measurement accuracy, particularly in 2-wire configurations, and shielding or routing practices may be needed depending on the installation environment.
The wiring architecture itself is a practical factor in selection — not just a matter of the sensor's electrical isolation, but of what cable routing is feasible at the installation site.
Multi-Point Temperature Monitoring
With fiber optic sensing, one point probe generally corresponds to one defined temperature measurement point. Multiple probes connect to a multi-channel temperature transmitter or monitoring instrument, forming a fiber optic temperature monitoring system.
Multiple PT100 elements can also be connected to multi-channel acquisition or control systems. The comparison here is less about whether multi-point monitoring is possible with either technology, and more about sensor wiring, channel quantity, instrument architecture and electrical isolation needs at each point.
| Requirement | Fiber Optic Approach | PT100 Approach |
|---|---|---|
| Single Point | One probe to one instrument channel | One RTD to one input channel |
| Several Points | Multiple probes to a multi-channel instrument | Multiple RTDs to a multi-channel module |
| Many Equipment Points | Multi-channel monitoring instrument with electrical isolation at each point | Multi-channel RTD acquisition system |
| PLC / SCADA Integration | Via monitoring instrument output | Via transmitter or RTD input module |
PLC, SCADA and Monitoring System Integration
Whether the sensing technology is PT100 or fiber optic, the measurement ultimately connects to a control system through a suitable transmitter or monitoring instrument.
Fiber optic monitoring instruments may provide RS485, Modbus RTU, analog output, alarm relay outputs and local display, depending on the specific instrument selected. PT100 measurements are typically brought into a control system through an RTD input module, a temperature transmitter, or a PLC with direct RTD/analog input, then integrated into the monitoring system.
The integration method differs between the two technologies, but both can be used in modern industrial monitoring systems.
Where PT100 Is Often the Practical Choice
PT100 remains a practical and familiar option for a wide range of applications, including conventional industrial machinery, process equipment, HVAC systems, tanks and piping, and bearing housings.
PT100 is often a practical choice when:
Electrical isolation is not a primary requirement EMI conditions are manageable Conventional wired sensor installation is acceptable Existing PLC or transmitter infrastructure already supports RTD inputs A standard industrial probe construction fits the measurement point
Where Fiber Optic Temperature Sensing Is Often Preferred
Fiber optic point temperature sensing is commonly used in transformer windings (both dry-type and oil-immersed), high-voltage equipment, generator windings, RF and microwave environments, MRI systems, and high-voltage testing setups.
These environments can make optical sensing more attractive because the measurement link does not rely on conductive signal wiring at the sensing point — offering electrical isolation, EMI immunity, a compact probe footprint, and connection to a remote monitoring instrument.
Fiber Optic vs PT100 by Application
| Application | Fiber Optic | PT100 | Main Selection Consideration |
|---|---|---|---|
| Transformer Winding | Often preferred | Depends on installation | Electrical isolation at the winding |
| Dry-Type Transformer | Often preferred | Depends on installation | EMI and voltage proximity |
| Switchgear | Common option | Common option | Location relative to energized parts |
| Busbar Connection | Often preferred | Depends on installation | Proximity to high current / voltage |
| Motor / Generator | Common option | Common option | Winding access and EMI level |
| Industrial Machinery | Depends on installation | Common option | Conventional wiring feasibility |
| Process Equipment | Depends on installation | Common option | Existing instrumentation |
| Microwave / RF | Often preferred | Suitable with correct design | RF interference with wiring |
| MRI / Strong Magnetic Field | Often preferred | Suitable with correct design | Magnetic field interaction |
| High-Voltage Testing | Often preferred | Suitable with correct design | Direct proximity to high voltage |
| Laboratory Test Bench | Common option | Common option | Flexibility and existing setup |
How to Choose Between a Fiber Optic Temperature Sensor and PT100
Use a PT100 when:
The measurement environment is electrically conventional Standard sensor wiring is acceptable Existing instrumentation already supports RTD inputs A conventional industrial probe fits the sensing point Electrical isolation at the measurement point is not a key requirement
Consider fiber optic sensing when:
The sensor is close to high voltage Direct electrical isolation is important Strong EMI / RFI is present RF or microwave fields are involved Strong magnetic fields are present Conductive sensor wiring is undesirable The sensing location is inside transformer or electrical winding structures
Questions to Ask Before Choosing PT100 or Fiber Optic Sensing
What temperature range is required? Where is the actual sensing point? Is the measurement location energized? Is electrical isolation required? Is strong EMI or RF present? Is a non-metallic probe required? How much installation space is available? How far is the monitoring instrument from the sensing point? How many points need to be monitored? Does the control system accept RTD input directly? Is RS485 / Modbus required? Is 4–20 mA required? Are alarm relay outputs required? Is local display required?
Common Misunderstandings When Comparing Fiber Optic Sensors and PT100
"Fiber optic sensors are always more accurate." Not necessarily. Accuracy depends on the complete sensor and instrument configuration, not on the sensing technology alone.
"PT100 cannot be used in electrical equipment." Incorrect. PT100 is widely used in electrical and industrial equipment; suitability depends on insulation, wiring and measurement location.
"Fiber optic sensing is only for transformers." It is also used in RF, microwave, generators, high-voltage testing, MRI and industrial test environments.
"Only the sensor specification matters." Probe structure, cable or fiber routing, channel count and monitoring interface are also part of the selection.